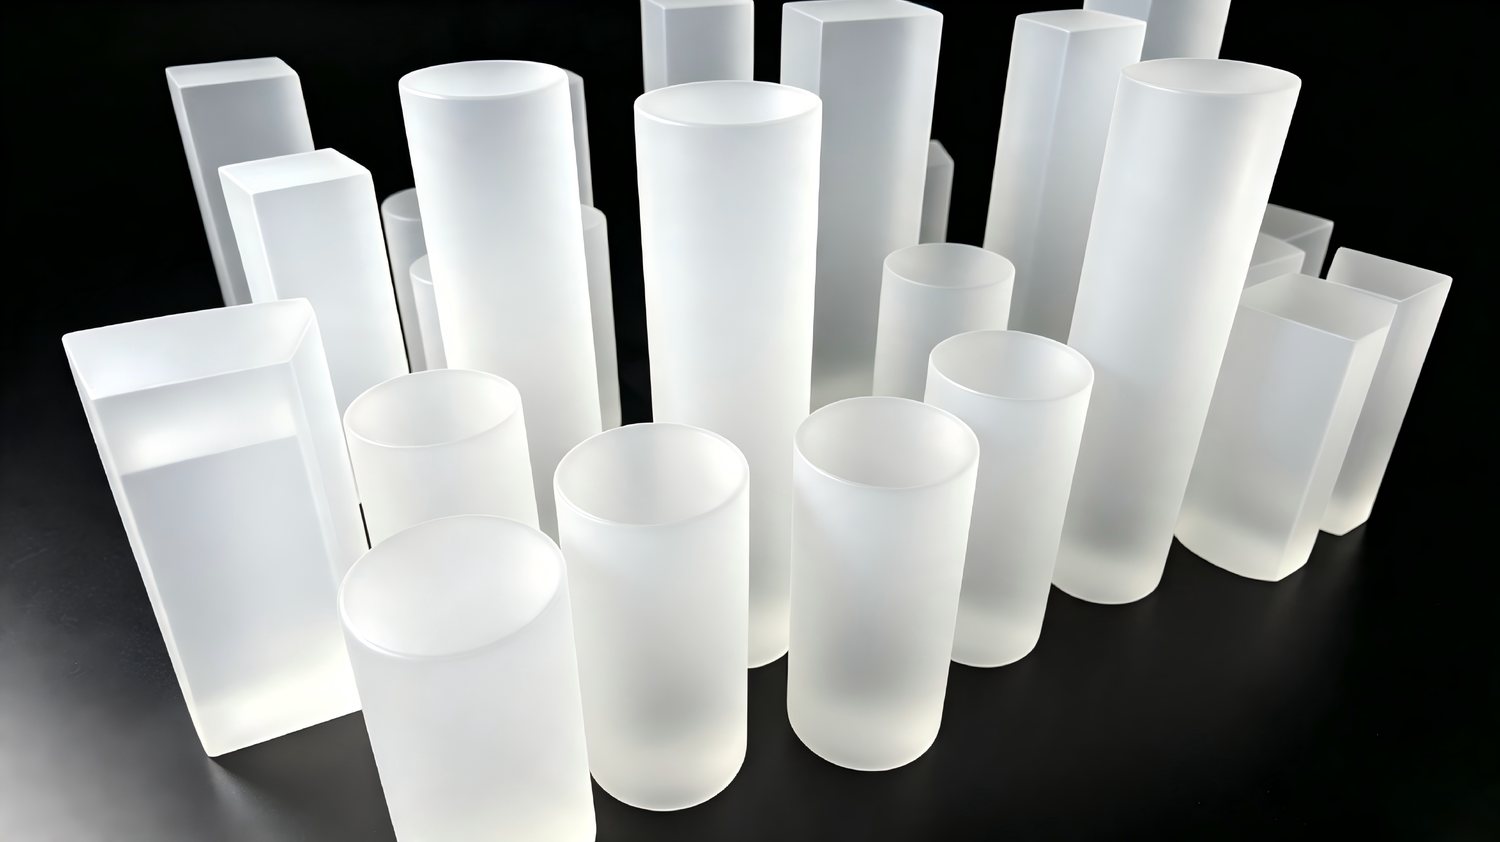
Frosted and machined acrylic cylinders in graduated sizes
Frosted and machined acrylic cylinders in graduated sizes
This page answers whether a machined acrylic supplier can produce precision rings and tubes from PMMA, and what tolerance, material and repeatability to expect for cylindrical parts.
Reply within 12 hours · free DFM feedback
Tolerances are confirmed per drawing and first article; concentricity and wall variation are quoted per feature.
Company-declared
Precision acrylic rings and tubes are CNC-machined from cast sheet, block and tube stock for spacers, bearing windows, insulators, roller covers, housings and optical details.
Cast acrylic recommended for machining-heavy parts, extruded for flat sheet: cylindrical machined parts are quoted in cast for cleaner edges and more stable machining.
Frosted and machined acrylic cylinders in graduated sizes
Fabricated acrylic thickness range 3–100 mm covers ring and tube walls; typical wall thicknesses run 3–20 mm and lengths are confirmed per part and stock size.
Rings and tubes use General tolerances per GB/T 1804-2000 / ISO 2768 varying with size span; Machined features to ±0.1 mm (holes and machined features) cover bores and ODs, and Critical dimensions on the 5-axis CNC to ±0.05 mm are verified at first article per drawing.

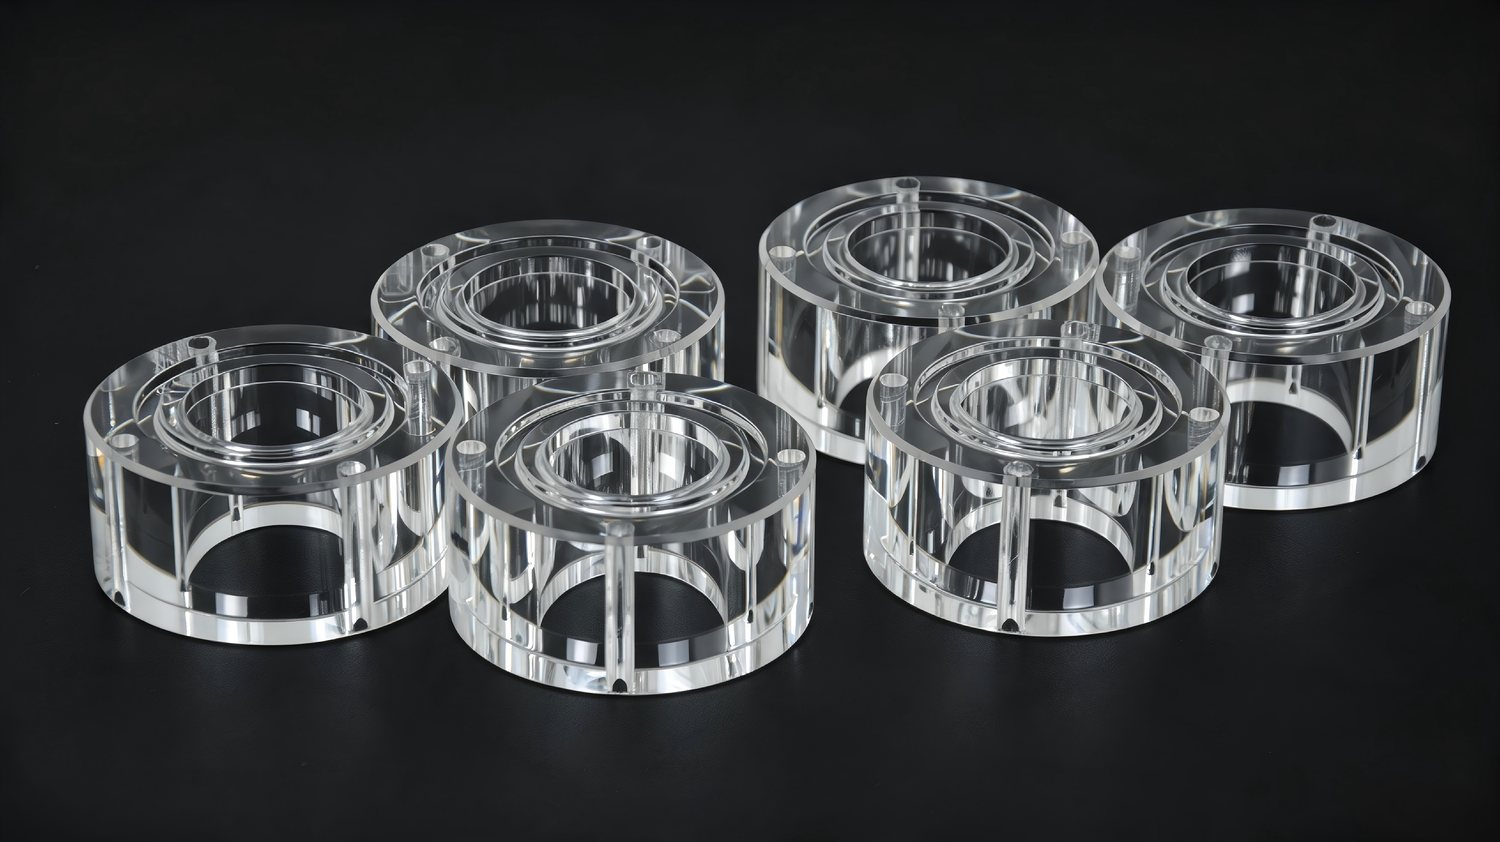
Precision-machined clear acrylic rotor housing
Visible faces follow Appearance described as clear / glass-clear / optically clear against the approved master sample, with faces polished where visible.
Drawings accepted as STEP/DWG/DXF/PDF/sketches; without a CAD file, a manufacturing drawing is prepared from the sketch.
Repeat runs stay consistent: First-article data retained; reorders run on the same CNC programs, and material locked to the part number for reorders.
Machined parts annealed with the cast-acrylic industry–standard schedule; rings and tubes are stress-relieved with this cycle after turning and milling, and temperature and soak values are confirmed per grade, not published. Annealing reduces but does not eliminate cracking risk under press fits, fasteners or solvents.
Typical ring and tube quantities follow Engineering review and quote within 12 hours on working days; Sample in 48 hours, production runs in 7 days.
Bonded joints described as near-invisible seams apply where ring stacks or tube assemblies are bonded into units.
Calypto cast acrylic sheet, cast in our own Suzhou facility, is the sourcing statement for our clear machined grades; Mitsubishi or Lucite optical-grade PMMA is supplied when the order specifies a branded material, confirmed per order.
| Choose this when | Do not choose this when | Option | Claim IDs |
|---|---|---|---|
| The part is machined cylindrical with tight bores | The part is a simple flat washer | Cast acrylic, CNC-machined | AF-C15 |
| Optical clarity matters | The part is a hidden spacer | Clear cast grade with polished faces | AF-C16 |
| The part repeats across orders | This is a one-off prototype | Program retention plus material lock | AF-C11, AF-C12 |
| The ring must press-fit over a shaft | The ring is a free-standing spacer | Fit tolerance confirmed per drawing and first article |
| Property | Value | Unit | Product grade | Thickness specimen | Test method / standard | Evidence status | Qualification | Claim IDs |
|---|---|---|---|---|---|---|---|---|
| Wall thickness | 3–20 mm typical; 3–100 mm capability | mm | Cast acrylic | Per part | Per drawing | company-declared | Confirmed per OD, ID and stock | AF-C05 |
| Machined tolerance | ±0.1 mm bores and ODs; ±0.05 mm drawing-flagged critical | mm | Fabricated parts | Per order | GB/T 1804-2000 / ISO 2768 plus first-article | company-declared | Per drawing, never a whole-part band | AF-C01, AF-C02, AF-C03 |
| Drawing formats | STEP, IGES, DWG, DXF, PDF or dimensioned sketch | n/a | Fabricated parts | Per order | Drawing review | company-declared | Manufacturing drawing drafted from sketches | AF-C14 |
| Repeatability | Same programs and locked material for reorders | n/a | Fabricated parts | Per part number | First-article retention | company-declared | Revision changes trigger a new first article | AF-C11, AF-C12 |
| Appearance | Polished faces where visible | n/a | Fabricated parts | Per order | Appearance acceptance standard | company-declared | A/B faces per master sample | AF-C16 |
| Lead time | Quote 12 h, sample 48 h, production 7 days | hours / days | Typical ring and tube quantities | Per order | Working hours Mon–Sat 09:00–18:00 GMT+8 | company-declared | Volume orders evaluated separately | AF-C09, AF-C13 |
Yes: rings and tubes are CNC-machined from cast sheet, block and tube stock, with bores and ODs at ±0.1 mm typical and drawing-flagged critical dimensions confirmed at ±0.05 mm by first-article inspection.
Typical walls run 3–20 mm inside the fabricated acrylic thickness range 3–100 mm, confirmed per OD, ID and stock at quoting.
First-article data retained; reorders run on the same CNC programs, and material locked to the part number for reorders keeps cylindrical features consistent.
Cast acrylic recommended for machining-heavy parts: cylindrical parts are machined from cast for cleaner edges and more stable machining.
Fit tolerances are confirmed per drawing and first article; concentricity and wall variation are quoted per feature rather than as a blanket band.
Precision acrylic rings and tubes are CNC-machined from cast sheet, block and tube stock for spacers, bearing windows, insulators, roller covers, housings and optical details. Cast acrylic is recommended for cylindrical machined parts for cleaner edges and more stable machining.
Rings and tubes use general tolerances per GB/T 1804-2000 / ISO 2768 varying with size span; ±0.1 mm covers bores and ODs, and ±0.05 mm applies only to drawing-called critical dimensions verified at first article. Concentricity and wall variation are quoted per feature, not as a blanket band.
First-article data is retained and reorders run on the same CNC programs with the material grade locked to the part number, so an approved reorder is inspected against the original first article. Press-fit and mating surfaces are confirmed per drawing and first article before production.
Send your drawing — an engineer replies within 12 hours.